Skip to content
ALLOT TECH5 GALLONWATERFilling machine solutions

Connected large-bottle equipment

Complete 5 Gallon Water Bottling Line: Equipment and Interfaces

A complete 5 gallon water bottling line connects bottle preparation, washing, filling, capping and the chosen finished-bottle route. A 3-in-1 washer-filler-capper is the core machine, not automatically the whole quoted line. Define each module and handover for your actual 18.9L or separately approved 20L bottle.

18.9L ≠ 20LReturnable + one-way pathsConfirmed / Reference / TBC
ALLOT TECH / LARGE-FORMAT WATERSYSTEM
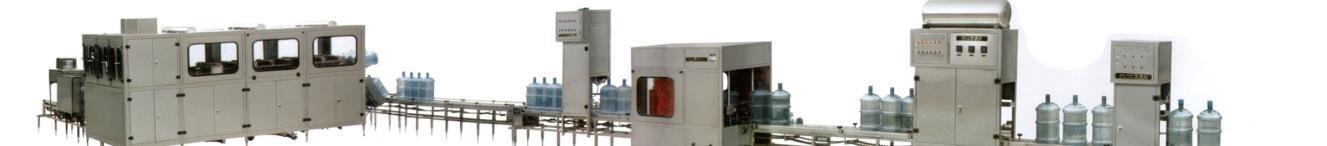
5 gallon water bottle washing filling and capping equipment reference
Real equipment reference. Final configuration is project-specific.

Decision summary

Use this page when the decision matches your project

A complete 5 gallon water bottling line connects bottle preparation, washing, filling, capping and the chosen finished-bottle route. A 3-in-1 washer-filler-capper is the core machine, not automatically the whole quoted line. Define each module and handover for your actual 18.9L or separately approved 20L bottle.

Suitable for
  • Large-format water operations specifying one connected equipment cell
  • Existing plants replacing disconnected bottle-handling machines
  • Delivery businesses planning bottle preparation and final handling
Not suitable for
  • Plant feasibility, permits or building design
  • Buyers needing only a replacement capper or washer
  • Small-bottle PET production
Required inputs
  • Returnable or one-way bottle flow
  • Bottle arrival and rejection condition
  • Required BPH and shift plan
  • Packing, rack or pallet route

Included equipment and handover map

What belongs in your complete-line quotation?

Use one row per task. Mark the quoted machine, manual work, buyer-supplied equipment or exclusion explicitly; the word complete does not settle the scope.

Equipment taskScope to identifyHandover to agreeEvidence before approval
Incoming bottle preparationInspection, old-cap removal, outside brushing and any approved pre-wash for the actual returnsAcceptable incoming bottle condition, feed direction and rejected-bottle removalReturned-bottle examples and a preparation module list
Internal washing and rinsingStages, bottle holders, nozzles, tanks, pumps and manual loading if retainedBottle orientation into the washer and controlled transfer toward fillingStage schedule, sample coverage review and transfer drawing
FillingFiller, approved bottle formats, product-water handover and relevant controlsBottle arrival, supply readiness and empty-bottle or no-water responseWritten filling basis and agreed response checks
Cap feeding and applicationSorter, feed route, treatment if specified, capper and manual replenishmentApproved neck and cap pair, cap availability and missing-cap responseCap samples, feeding trial and closure acceptance method
Finished-bottle checksVisual checks, sensors or tests actually included; do not assume one sensor verifies everythingRejected-bottle identification, removal and agreed release responsibilityDefined defects, detection limits and witnessed rejection checks
Discharge and packagingConveyors, bagging, handles, racks or pallet handling actually selectedBottle orientation, receiver availability, local buffer and blocked-discharge responseRepresentative packaging samples and a connected transfer trial

Use boundary: This scope stops at the agreed equipment-cell boundaries. Treatment design, buildings, warehouses, permits and other plant services are not implied inclusions.

Reusable buying worksheet

Send one clear machine requirement

Download the editable CSV worksheet for bottle, cap, capacity, wash process, equipment inclusions and quotation terms. Fill what you know; leave unknown items marked “to be confirmed.”

Download RFQ Worksheet (CSV)

No registration is needed. The download sends no inquiry automatically. Review your entries, then use the proposal form or the contact details on this page. For the form, paste the relevant answers into the project description; CSV uploads are not accepted.

01

Start with the returned-bottle route

For a returnable-bottle project, map receiving and inspection, old-cap removal, external cleaning, the approved internal wash and final-rinse sequence, filling, capping, finished checks and discharge. Identify where an unsuitable bottle leaves the route. The detailed stages depend on the accepted return condition; a longer equipment list is not proof of better cleaning.

  • Separate normal returned bottles from the worst condition the process will accept
  • Show every manual lift or transfer between quoted modules
  • Keep the dirty-to-clean transition visible on the equipment drawing
  • Agree the wash-validation responsibility separately from mechanical acceptance
02

What changes for new one-way bottles?

New bottles do not need used-cap removal, but they still need a defined receiving, unpacking, inspection and preparation method. Bottle material, geometry, packaging and the approved process decide which modules can be omitted or changed. New does not automatically mean ready to fill.

  • Confirm the condition in which the bottle supplier delivers containers
  • Define unpacking and feeding work, including manual tasks
  • Approve the actual bottle and cap instead of relying on the nominal volume
  • Keep purchased-bottle supply and any bottle-forming equipment as explicit scope choices
03

Connect machines, not just matching BPH labels

Two machines with the same nominal bottles-per-hour label can still have incompatible transfer heights, bottle orientation, operating cycles or control signals. Request a handover drawing and a named integration owner for every boundary, especially when retaining equipment from another supplier.

  • Record transfer height, direction, bottle support and the accepted format
  • State reference output and operator tasks on the same bottle and process basis
  • Identify ready, run-permit, fault and receiver-full signals where applicable
  • Request the interface details of existing equipment before assuming reuse
  • Verify transfers with representative bottles under an agreed connected test
04

Agree the connected stop and restart checks

Include cap starvation, loss of product-water readiness, unavailable downstream equipment and rejected-bottle handling in the agreed cause-and-effect review. The supplier should state which modules pause, how bottles already in process are handled and what permits restart. Qualified personnel should conduct approved tests without bypassing guards or safety devices.

  • Distinguish a normal process stop from the separately validated safety system
  • Define whether in-process bottles need reinspection or removal after an interruption
  • Record signals, expected response and actual result during the connected trial
  • If equipment cannot be tested together at FAT, name the remaining site-acceptance checks
05

Get one coordinated scope before comparing quotations

Ask for a module list, equipment arrangement, connection schedule, interface responsibilities and acceptance plan that describe the same configuration. These documents turn an attractive line picture into a scope that can be compared. They do not replace plant-wide civil design, licensing, laboratory planning or qualified local engineering.

  • Identify included, optional, buyer-supplied and excluded equipment separately
  • Mark preliminary assumptions and the evidence needed to close them
  • Separate machine cost, preparation options and finished-bottle handling subtotals
  • State who supplies connecting conveyors, piping, wiring and commissioning work
  • Use the RFQ worksheet with bottle details, required output and existing-equipment information
Q / INPUT

Information needed for a quote

Send the bottle and cap basis, required BPH, bottle path, factory and utility information, destination and any module or support requirement. Unknown items can remain marked “to be confirmed.”

Request a Connected Equipment Scope

FAQ

Short answers, visible boundaries

Project-specific output, hygiene, utilities and service terms belong in the confirmed technical proposal.

Is a 3-in-1 filling machine a complete 5 gallon line?

It integrates the quoted washing, filling and capping functions. Returned-bottle inspection, decapping, outside brushing, connecting conveyors and finished-bottle handling are separate scope questions unless explicitly included.

Does a complete line always include water treatment?

No. Water treatment is a separate connected system that requires raw-water and finished-water data. The filling-line proposal should define only its product-water handover interface unless treatment is explicitly included.

Can I reuse an existing decapper, washer or conveyor?

Possibly. Provide its bottle basis, dimensions, transfer height and direction, reference rate, controls and condition. Compatibility and responsibility for modifications need a review; matching BPH alone is not approval.

Can packaging automation be added later?

Potentially, if the initial layout, discharge position, control interfaces and utility provision support the named future module. Do not assume every machine can be expanded without modification.

What proves that the quoted machines work together?

An agreed connected trial using approved bottles, caps and relevant packaging can verify transfers and defined responses. Record the operating conditions, output basis, deviations and any checks deferred to site acceptance. A model list or separate machine videos is not that test.

Prepared by

Allot Tech Content & Project Coordination
Last reviewed: 2026-09-28. Technical values follow Confirmed, Reference or To Be Confirmed status. Catalog conflicts are disclosed; the signed quotation and technical agreement control the final project.

Contextual next step

Request a Connected Equipment Scope

Send the bottle, cap, output and factory basis. Unknown values can remain open instead of being invented.