Skip to content
ALLOT TECH5 GALLONWATERFilling machine solutions

Bottle reuse decision

5 Gallon Bottle Inspection and Leak Testing

Bottle inspection and leak testing determine whether a returned large-format bottle should continue into washing and filling. Rejection rules belong to the plant quality system and local requirements.

18.9L ≠ 20LReturnable + one-way pathsConfirmed / Reference / TBC
ALLOT TECH / LARGE-FORMAT WATERSYSTEM
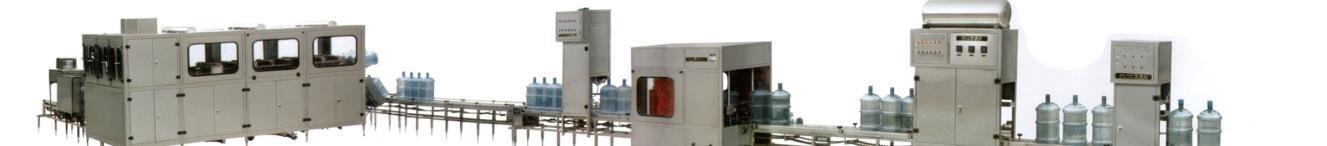
5 gallon water bottle washing filling and capping equipment reference
Real equipment reference. Final configuration is project-specific.

Decision summary

Use this page when the decision matches your project

Bottle inspection and leak testing determine whether a returned large-format bottle should continue into washing and filling. Rejection rules belong to the plant quality system and local requirements.

Suitable for
  • Returnable bottle fleets
  • Plants with recurring crack, neck or leakage issues
  • Operations formalizing rejection records
Not suitable for
  • Using equipment as a substitute for quality procedures
  • Inventing a universal reject threshold
  • Filling visibly unacceptable bottles
Required inputs
  • Known bottle failure modes
  • Local quality requirements
  • Manual inspection points
  • Desired automatic test and reject integration

Detection scope and limits

Visual inspection, leak testing and contamination checks are different tasks

Specify each required check and prove it with approved reference samples. A pass at one station cannot replace the other acceptance decisions.

Buyer concernCheck to specifyEvidence to requestWhat a pass does not prove
Visible body, base or neck damageDefined manual or camera inspection with controlled presentationApproved defect examples, lighting and views, accepted/rejected sample recordNo guarantee of detecting hidden damage or non-visible contamination
Bottle integrity or leakageBottle-specific leak method and approved test conditionsReference sound and defective bottles; repeat trials and reject confirmationDoes not establish cleaning effectiveness, odor or microbiological safety
Foreign residue, suspicious history or odorSegregation and quality-team assessment; a separately specified detection method if requiredWritten hold/reject policy and method limitationsOrdinary cameras and a leak test do not establish absence of odor or chemical contamination
Cap/neck sealing after fillingFilled-bottle closure checks defined for the actual cap and neckApproved cap lot, application settings and seal-test recordsAn empty-bottle leak result does not approve the applied closure
Reliable removal of failed bottlesTracking, reject action and confirmation under the agreed operating conditionsRejected sample reconciled with the station record and physical reject locationA screen alarm alone does not prove removal from the production stream

Use boundary: Detection technologies, thresholds and test conditions remain subject to the approved equipment proposal. This table does not claim that every function is included in a standard QGF machine.

01

Visual inspection scope

Visual inspection addresses visible defects such as cracks, deep scratches, deformation, neck damage and visible foreign matter. Lighting, rotation and presentation affect what can be seen. An ordinary camera does not detect odor; suspect chemical exposure or unknown residues require segregation and assessment under the approved quality procedure.

  • Body and base
  • Shoulder and handle
  • Neck finish and visible foreign matter
  • Separate non-visual contamination assessment
  • Documented visible-defect limits
02

Leak and integrity testing

A selected leak test should match bottle material, deformation and line speed. The proposal must define the method, bottle presentation, reject action and test limitations rather than implying perfect detection.

  • Test method to be confirmed
  • Reference bottle set
  • False-reject handling
  • Failed-bottle discharge
  • Verification and maintenance checks
03

Manual versus automatic inspection

Manual inspection depends on lighting, training, presentation and sustainable operating pace. Automatic systems can improve repeatability for the defects the selected method is designed and demonstrated to detect. Keep visual, leak and any specialized contamination-detection scope separate in the equipment agreement.

  • Operator workload
  • Defined detectable defects
  • Bottle rotation or spacing
  • Reject confirmation
  • Recordkeeping
04

Prepare a safe challenge-sample test

Have the responsible engineer and quality team approve a controlled set of identified sound bottles and reference defects before the trial. Record the expected classification and compare it with the detection result and actual reject route. Do not improvise hazardous contamination or unsafe pressure tests. Test settings and sample preparation must follow the selected equipment and approved procedure.

  • Sound samples from each approved bottle format
  • Controlled reference defects approved for the test
  • Expected versus observed result for each sample ID
  • Sound bottles rejected and defect samples accepted recorded separately
  • Repeat checks after changes with the original results retained
05

Write plant-specific reject logic

The quality team should approve defect categories, disposition, traceability and escalation under local rules. Machine alarms and reject stations should support that policy.

  • Accept, hold and reject categories
  • Segregated reject area
  • Root-cause review
  • Bottle fleet replacement
  • Local compliance confirmation
Q / INPUT

Information needed for a quote

Send the bottle and cap basis, required BPH, bottle path, factory and utility information, destination and any module or support requirement. Unknown items can remain marked “to be confirmed.”

Request a Configuration-Based Proposal

FAQ

Short answers, visible boundaries

Project-specific output, hygiene, utilities and service terms belong in the confirmed technical proposal.

Can a leak test confirm that a returned bottle is clean?

No. A leak test evaluates integrity under its stated method and conditions. Cleaning and contamination acceptance require separate approved checks.

Can a camera detect odor inside a bottle?

An ordinary visual-inspection camera cannot detect odor. Specify a separate assessment or suitable detection method where required, and do not assume that it is included.

Can a leak tester detect every damaged bottle?

No test should be assumed to detect every defect. The confirmed method and limitations must be understood alongside visual and hygiene inspection.

Should scratched bottles be rejected?

The plant should define its own criteria according to bottle condition, local requirements and quality policy.

Where should rejected bottles go?

Use a controlled, segregated route that prevents rejected bottles from returning unnoticed to the clean production flow.

Prepared by

Allot Tech Content & Project Coordination
Last reviewed: 2026-09-22. Technical values follow Confirmed, Reference or To Be Confirmed status. Catalog conflicts are disclosed; the signed quotation and technical agreement control the final project.

Contextual next step

Request a Configuration-Based Proposal

Send the bottle, cap, output and factory basis. Unknown values can remain open instead of being invented.