Skip to content
ALLOT TECH5 GALLONWATERFilling machine solutions

Buyer guide / pre-shipment test

FAT Checklist for a 5 Gallon Water Filling Machine

A FAT checklist converts the technical agreement into observable tests. It should name the approved bottle and cap, test conditions, measurement method, documents and responsibility for open items.

18.9L ≠ 20LReturnable + one-way pathsConfirmed / Reference / TBC
ALLOT TECH / LARGE-FORMAT WATERGUIDE
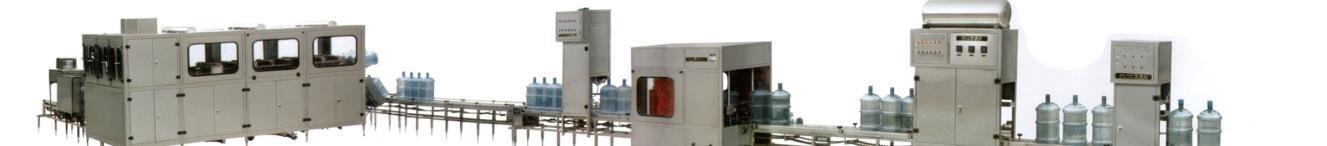
5 gallon water bottle washing filling and capping equipment reference
Real equipment reference. Final configuration is project-specific.

Decision summary

Use this page when the decision matches your project

A FAT checklist converts the technical agreement into observable tests. It should name the approved bottle and cap, test conditions, measurement method, documents and responsibility for open items.

Suitable for
  • Buyers preparing factory acceptance
  • Inspectors reviewing machine evidence
  • Projects with signed technical specifications
Not suitable for
  • Using a generic video as acceptance
  • Testing unapproved samples
  • Ignoring utility conditions and deviations
Required inputs
  • Contract and technical attachment
  • Approved bottles and caps
  • Test duration and method
  • Required documents and spares

Witnessed test record

What to record during a 5 gallon machine FAT

Use the signed technical agreement to fill the acceptance requirement, result, evidence reference, status and owner for each row. Do not pre-mark a result as passed.

Test recordIdentify before the testEvidence to retainDecision or open item
Machine and sample identityMachine/configuration revision; bottle format and sample IDs; cap lotScope check, sample approval and drawing referencesRecord substitutions or untested formats
Utilities and programMeasured supply conditions, wash program and instrument basisUtility readings and agreed program revisionList differences from the destination site
Handling and sequenceApproved feeding, turning, transfer, drainage and discharge methodObserved sequence with sample and time referencesAssign each handling exception and required change
Output, fill and closureMeasurement window, count point, fill method and closure acceptance ruleElapsed time, accepted count, rejects, stops and measured sample resultsCompare only against the agreed requirement
Detection and reject routeApproved safe challenge set and expected classificationsSample-by-sample detection and physical removal recordSeparate false acceptance, false rejection and reject-route failures
Alarms and safety functionsApproved test procedure performed by qualified personnelFunction tested, expected response, observed response and restart recordNo bypass of safeguards; resolve safety-related open items
Documents and closeoutDocument revisions, ordered spares and release requirementsSigned results and linked punch-list items with retest evidenceNamed decision owner and agreed shipping-release status

Use boundary: FAT verifies the agreed factory test scope under recorded conditions. It does not replace destination-site commissioning, sanitation validation or local compliance approval.

01

Prepare before the test

Confirm the machine configuration, drawing revision, test samples, cap lot, utilities, instruments, people and open deviations. Record any difference from final site conditions.

  • Specification revision
  • Sample approval
  • Utility record
  • Measuring tools
  • Test responsibility
02

Check machine and sequence

Inspect ordered components and accessible surfaces, then run dry and wet cycles. Observe bottle transfer, washing, filling, cap feed, capping and finished-bottle discharge.

  • Appearance and ordered scope
  • Dry run
  • Water test
  • Bottle transfer
  • Fill and cap result
03

Agree the output count and measurement window

Identify a single count point and record the elapsed test time, accepted bottles, rejected bottles and stops. Accepted BPH equals accepted bottles divided by elapsed test hours. State how startup and planned interruptions are treated before testing; do not remove unplanned stops afterward to improve the result. A short run does not demonstrate sustained shift output.

  • Start and end time with a defined count point
  • Accepted and rejected bottle counts kept separate
  • Stops recorded with duration and reason
  • Fill and closure results tied to the tested bottle and cap lot
  • Agreed trial duration rather than an implied universal duration
04

Test abnormal conditions

Qualified personnel should check the contracted alarm and safety functions using an approved test procedure. This may cover missing bottle, cap shortage, blocked outfeed, guard opening, emergency stop and controlled restart. Do not improvise tests, defeat safeguards or reach into moving equipment.

  • Approved procedure and responsible test leader
  • No-bottle and cap-shortage logic where included
  • Blocked-discharge response
  • Safety-function evidence and controlled restart
  • Observed response and unresolved deviations
05

Keep failed results when recording a retest

Give each open item an ID, requirement reference, observed result, owner and agreed next action. Link any change and retest to the original record instead of replacing it with a pass. State whether the item blocks release or requires a documented later verification under the agreed release process.

  • Original result and evidence reference
  • Change made and configuration revision
  • Retest conditions and result
  • Remaining site verification where applicable
  • Release decision and authorized owner
06

Close evidence and packing

Record capacity under the agreed method, rejects and stops, documents, spare parts and punch-list actions. Inspect packing only after release criteria are met.

  • Signed result
  • Capacity basis
  • Punch list
  • Documents and backups
  • Packing inspection
Q / INPUT

Information needed for a quote

Send the bottle and cap basis, required BPH, bottle path, factory and utility information, destination and any module or support requirement. Unknown items can remain marked “to be confirmed.”

Request a Configuration-Based Proposal

FAQ

Short answers, visible boundaries

Project-specific output, hygiene, utilities and service terms belong in the confirmed technical proposal.

Can the FAT checklist change after the order?

Changes should be agreed by both parties. The contract and technical attachment control the final scope.

Should FAT use used returnable bottles?

Use the approved sample set defined for the test, which may include representative returned bottles when relevant.

What is a punch list?

It records open items, owners, evidence and due dates after the test.

Prepared by

Allot Tech Content & Project Coordination
Last reviewed: 2026-09-22. Technical values follow Confirmed, Reference or To Be Confirmed status. Catalog conflicts are disclosed; the signed quotation and technical agreement control the final project.

Contextual next step

Request a Configuration-Based Proposal

Send the bottle, cap, output and factory basis. Unknown values can remain open instead of being invented.