Skip to content
ALLOT TECH5 GALLONWATERFilling machine solutions

Buyer guide / hygiene configuration

How Many Washing Stages Does a Returnable Bottle Line Need?

There is no universal washing-stage count for every returnable bottle line. The correct sequence depends on incoming bottle condition, local requirements, cleaning validation and the selected equipment.

18.9L ≠ 20LReturnable + one-way pathsConfirmed / Reference / TBC
ALLOT TECH / LARGE-FORMAT WATERGUIDE
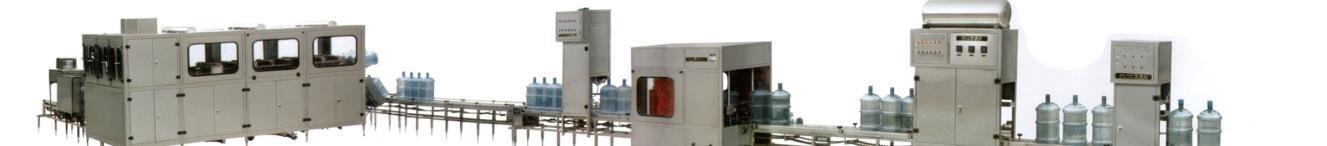
5 gallon water bottle washing filling and capping equipment reference
Real equipment reference. Final configuration is project-specific.

Decision summary

Use this page when the decision matches your project

There is no universal washing-stage count for every returnable bottle line. The correct sequence depends on incoming bottle condition, local requirements, cleaning validation and the selected equipment.

Suitable for
  • Returnable-bottle plants
  • Projects comparing wash configurations
  • Hygiene teams preparing validation
Not suitable for
  • Copying fixed chemical recipes
  • Skipping bottle inspection
  • Assuming more stages automatically means a better result
Required inputs
  • Returned-bottle sample set
  • Local hygiene requirements
  • Water and drain conditions
  • Machine stage options

Compare the program, not the headline number

Six fields to request for every quoted washing stage

Use the same schedule for each proposal. A station count is not enough to compare two washing programs.

Schedule fieldRecord for each proposalQuestion it resolves
Function and positionPurpose of the step and physical positions usedAre the quoted stages separate functions or repeated stations?
Supply and return circuitLiquid source, tank, pump, return or drain routeWhich steps share a circuit and which are separate?
Actual exposure and drainageSpray/contact interval and separate movement/drain intervalsDoes the quoted program provide the agreed exposure at the proposed rate?
Coverage and presentationBottle orientation, nozzle arrangement and sample geometryHow is coverage evaluated for the actual bottle and handle?
Controls and monitoringAdjustable values, operator checks and stated alarm behaviorWho detects and responds to conditions outside the approved program?
Acceptance evidenceTrial method, observed exceptions and site-validation responsibilityWhat is demonstrated before shipment and what remains a site task?

Use boundary: This is a proposal-comparison schedule, not a cleaning recipe. Do not infer chemical concentration, temperature, contact time or hygiene performance from the number of rows or stations.

01

A stage, a station and a tank are not the same thing

A stage describes a process purpose. A station is a physical bottle position, and a tank is part of a liquid circuit. Several positions may repeat one operation or share one tank. Ask each supplier to mark its terminology on the sequence drawing before comparing a six-stage and a ten-stage offer.

  • Count distinct process functions separately from bottle positions
  • Identify repeated operations and shared tanks
  • Show movement and drain intervals as well as spray positions
  • Confirm whether external brushing is inside or outside the quoted count
02

Classify incoming bottles first

Separate normal return soil from bottles that should be rejected. Record old caps, labels, dust, internal residues, odor, deformation and route history rather than using only new bottles.

  • Normal return sample
  • Worst acceptable sample
  • Reject sample
  • Bottle material and age
  • Route and storage condition
03

Give every stage a function

A stage may loosen soil, wash, sanitize where required, rinse or provide a final qualified-water rinse. Avoid repeated stations that have no stated process purpose or acceptance point.

  • Pre-wash purpose
  • Wash purpose
  • Sanitizing purpose where selected
  • Rinse purpose
  • Drain and carryover control
04

Check time, coverage and recirculation

Stage count alone does not define cleaning. Spray-nozzle coverage, contact, bottle drainage, solution monitoring, tank access and refresh rules matter to the result.

  • Nozzle position
  • Bottle rotation or indexing
  • Tank and pump condition
  • Recipe adjustability
  • Final-rinse separation
05

Resolve a faster machine rate against the same wash program

On an indexing machine, a change in cycle timing can affect spray, contact, movement and drainage intervals. A higher nominal BPH should therefore be checked against the approved stage schedule, not selected independently. Ask the supplier to explain how the required program is retained and document any changes to positions, circuits or timing.

  • The rate used in the program trial
  • Exposure and drainage basis at that rate
  • Allowed adjustment range and control responsibility
  • Exceptions that require a new technical agreement
06

Validate the final program

Final cleaning parameters must be confirmed according to bottle condition, local regulations and the selected machine configuration. FAT checks the built sequence; site validation confirms the operating program under local conditions.

  • No universal chemistry
  • No universal concentration
  • No universal temperature
  • No universal contact time
  • Documented local approval
Q / INPUT

Information needed for a quote

Send the bottle and cap basis, required BPH, bottle path, factory and utility information, destination and any module or support requirement. Unknown items can remain marked “to be confirmed.”

Request a Configuration-Based Proposal

FAQ

Short answers, visible boundaries

Project-specific output, hygiene, utilities and service terms belong in the confirmed technical proposal.

Does a ten-stage washer have ten separate tanks?

Not necessarily. Stage, station and tank counts describe different things. Request a sequence and circuit schedule showing which positions share a liquid source or return.

Is a ten-stage washer always better than a six-stage washer?

Not automatically. Compare the purpose, coverage, control and validation of each stage.

Can the supplier choose the hygiene recipe alone?

The supplier can propose a configuration, but the plant and local requirements must confirm the operating program.

What can FAT prove?

It can verify machine sequence and functional performance under stated test conditions, not every local microbiological outcome.

Prepared by

Allot Tech Content & Project Coordination
Last reviewed: 2026-09-22. Technical values follow Confirmed, Reference or To Be Confirmed status. Catalog conflicts are disclosed; the signed quotation and technical agreement control the final project.

Contextual next step

Request a Configuration-Based Proposal

Send the bottle, cap, output and factory basis. Unknown values can remain open instead of being invented.