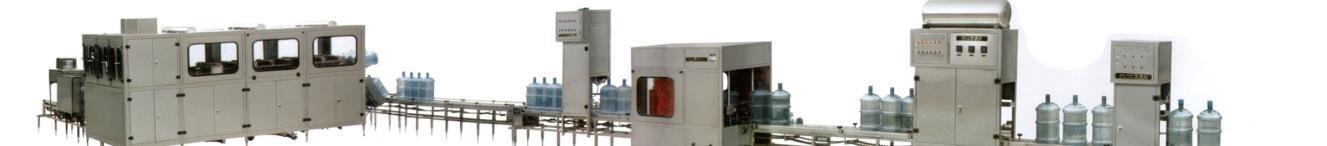
Specify the full-bottle conveyor interface
Provide actual filled mass, bottle-base shape, height and diameter for each format. Mark travel direction, transfer elevations and available space on the machine-cell drawing. Ask how guide settings, transitions and accumulation will be checked with full bottles, including any wet surface condition expected at the handover.
- Infeed and outfeed height with a common drawing datum
- Bottle support through transfers and changes of direction
- Permitted accumulation defined by the equipment supplier
- Access for inspection, drainage and safe maintenance
- Separate review for ramps, lifts or other elevation changes
Bagging is not the same as shrink packaging
A protective bag application does not by itself specify a shrink process. Provide the actual bag material and presentation requirement, and state whether closing, sealing or shrinking is requested. If a heated process is proposed, require the packaging and bottle/closure combination to be reviewed and trialed; do not assume every bag or filled bottle is suitable.
- Bag dimensions, material and supplied format
- Coverage and finished appearance agreed from samples
- Bag-feed, changeover and replenishment tasks
- Closure or heat equipment listed only when selected
- Separate proof for handle fit where a handle is requested
Rack loading and palletizing need different evidence
Use the actual delivery format as the starting point. A rack loader must place bottles into the approved pockets and orientation; a palletizing arrangement must follow an approved layer and load pattern. Define who provides racks, pallets, separators and any load-securing equipment. A generic robot or nominal payload figure is not proof of compatibility.
- Rack or pallet drawings and representative samples
- Bottle orientation, clearance and contact locations
- Full and empty carrier exchange responsibilities
- Approved completed-load criteria
- Site handling and structural checks by responsible specialists
Agree what happens when the outfeed stops
A bag change, rack exchange or full pallet can interrupt discharge even when the filler has available capacity. Request a cause-and-effect list for full accumulation, downstream not-ready, missing packaging and restart. The supplier should define where bottles wait and which upstream machines stop. This page addresses immediate machine interfaces, not plant-wide OEE optimization.
- Maximum accumulation and trigger location
- Stop and ready signals between supplied and existing equipment
- Operator clearance and restart method
- Guarding and emergency-stop interface ownership
- Witnessed controlled stop/restart tests without bypassing safety devices
Compare a staged upgrade on the same task basis
Compare manual, assisted and automatic options using the same bottle, required rate, material-replenishment tasks and transfer points. Identify which lifting or loading task changes, what remains manual and what later interfaces must be reserved. No universal output threshold establishes safe manual handling, operator count or financial payback.
- Current task and proposed replacement task
- Remaining operator duties and assessment responsibility
- Packaging consumption and changeover information
- Equipment-cell space and utility boundaries
- Installation and future interface items priced separately
Information needed for a quote
Send the bottle and cap basis, required BPH, bottle path, factory and utility information, destination and any module or support requirement. Unknown items can remain marked “to be confirmed.”
Request a Finished-Bottle Handling Scope