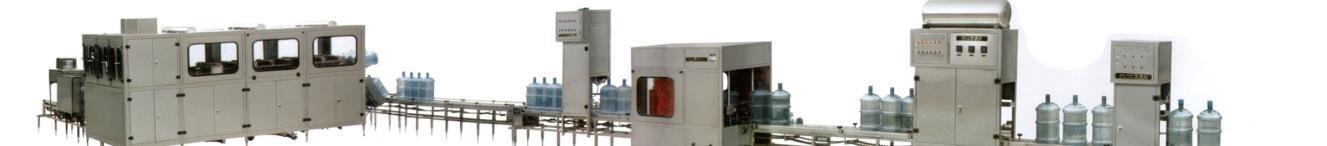
Visual inspection scope
Visual inspection addresses visible defects such as cracks, deep scratches, deformation, neck damage and visible foreign matter. Lighting, rotation and presentation affect what can be seen. An ordinary camera does not detect odor; suspect chemical exposure or unknown residues require segregation and assessment under the approved quality procedure.
- Body and base
- Shoulder and handle
- Neck finish and visible foreign matter
- Separate non-visual contamination assessment
- Documented visible-defect limits
Leak and integrity testing
A selected leak test should match bottle material, deformation and line speed. The proposal must define the method, bottle presentation, reject action and test limitations rather than implying perfect detection.
- Test method to be confirmed
- Reference bottle set
- False-reject handling
- Failed-bottle discharge
- Verification and maintenance checks
Manual versus automatic inspection
Manual inspection depends on lighting, training, presentation and sustainable operating pace. Automatic systems can improve repeatability for the defects the selected method is designed and demonstrated to detect. Keep visual, leak and any specialized contamination-detection scope separate in the equipment agreement.
- Operator workload
- Defined detectable defects
- Bottle rotation or spacing
- Reject confirmation
- Recordkeeping
Prepare a safe challenge-sample test
Have the responsible engineer and quality team approve a controlled set of identified sound bottles and reference defects before the trial. Record the expected classification and compare it with the detection result and actual reject route. Do not improvise hazardous contamination or unsafe pressure tests. Test settings and sample preparation must follow the selected equipment and approved procedure.
- Sound samples from each approved bottle format
- Controlled reference defects approved for the test
- Expected versus observed result for each sample ID
- Sound bottles rejected and defect samples accepted recorded separately
- Repeat checks after changes with the original results retained
Write plant-specific reject logic
The quality team should approve defect categories, disposition, traceability and escalation under local rules. Machine alarms and reject stations should support that policy.
- Accept, hold and reject categories
- Segregated reject area
- Root-cause review
- Bottle fleet replacement
- Local compliance confirmation
Information needed for a quote
Send the bottle and cap basis, required BPH, bottle path, factory and utility information, destination and any module or support requirement. Unknown items can remain marked “to be confirmed.”
Request a Configuration-Based Proposal